Gear Box Dowel Through Prop

Back to the purpose of this thread. Engine is back from the machine shop. Still has 1 dowel, the other one is still at the bottom of the lake. A few taps and the dowel came right out. The dowel is a slip fit in the block holes. Diameter measurements as follows:

Dowel - 0.6205"
Engine Block - 0.624-0.625"
Ox Gear - 0.630"

2.68 gear with reverse rotation, so the dowels and bolts see 1.68 torque magnification. Iron blocks will rust the dowel right in, not so much on aluminum.

No wonder it fell out :unsure:


I called ICT Billet to ask about their dowels; they told me 0.619 for the standard and 0.621 for the extended length.

This is what I am thinking. Order some 0.625 SST material and make some dowels with 1/4"-20 female thread tapped into one end. Press the dowels in with loctite and then hold them in with a 1/4-20 screw from the front side.
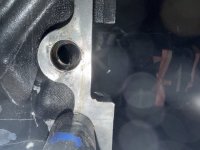
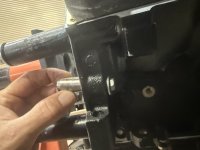
IMG_5385.jpeg

IMG_5388.jpeg


I scored a spare truck intake manifold for the price of a blown engine.
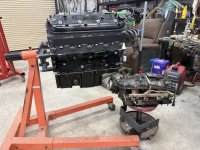
IMG_5386.jpeg
 
Back to the purpose of this thread. Engine is back from the machine shop. Still has 1 dowel, the other one is still at the bottom of the lake. A few taps and the dowel came right out. The dowel is a slip fit in the block holes. Diameter measurements as follows:

Dowel - 0.6205"
Engine Block - 0.624-0.625"
Ox Gear - 0.630"

2.68 gear with reverse rotation, so the dowels and bolts see 1.68 torque magnification. Iron blocks will rust the dowel right in, not so much on aluminum.

No wonder it fell out :unsure:


I called ICT Billet to ask about their dowels; they told me 0.619 for the standard and 0.621 for the extended length.

This is what I am thinking. Order some 0.625 SST material and make some dowels with 1/4"-20 female thread tapped into one end. Press the dowels in with loctite and then hold them in with a 1/4-20 screw from the front side.

View attachment 100271

View attachment 100272


I scored a spare truck intake manifold for the price of a blown engine.

View attachment 100270
Based on your experience, that is good reaction. I'm pretty sure that they should be a press fit to the block and a slip fit to the gearbox. If you make them .001 to .0015 oversize (measure the holes in the block you are putting them in) . Put a nice easy chamfer (15-20°) on the leading edge and drive them into the block. If you want to use an internal thread to pull them in or lock them in, you can go to 3/8 if you want. The dowels are primarily there for alignment because they make the holes in the bell housing / gear reduction loose to make them assemble easily. There should be enough clamp force in the bolted joint that the dowels are not really doing anything after assembly. This is probably why you had your rogue dowel catastrophe. Your dowels were too much undersize.
 
Don,

I have done some more investigation. You are correct that the purpose of them is for install/alignment and once clamped they really don't or shouldn't do anything. One option is to just remove them after the gear box is installed and clamped.

I got an Iron 6.0 and an aluminum 6.2 sitting side by side. SA says it's only an issue with Aluminum blocks, but more discussion says Iron sometimes too. All the dowels holes in both blocks are 0.624-0.625. I also have a grab bag of dowels that are all 0.620-0.621. The factory setup is a slip fit on everything.

I looked on McMaster, Pull out Dowels with pre threaded 5/16-18 holes are 0.625 +0.001-0.003. That is way too much press for this application and might split the Iron block ears.

Here is where I stand. I have two sets of these dowels coming next week. They have through holes for 5/16 bolts to act as keepers.

Food for thought, OX drive instructions say 0.005" max run out between gear drive plate and flex plate. That's basically everything machined perfect and the 0.010" dowel clearance fit on the box. I spent a whole afternoon last time making sure the two were concentric and nothing was pushing or pulling on the crank.

So, do all of this or punch them out after the gear box is installed is the question?? :unsure:


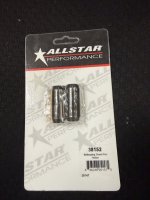
aaf-all38152_xl.jpg


https://www.summitracing.com/parts/AAF-ALL38152
 
Last edited:
.010 dowel clearance will allow you .010 runout if both holes are exactly the same distance apart. The thing about runout is that it doubles the position offset. What is the size of the dowel holes in the gear reduction? You can be reasonably sure that OxBox is holding the dowel holes to the input bore very close. I would think that they would be done in the same machining operation. According to the Machinery's Handbook you don't want more than .0016 interference with a cast iron OD. What is the PN of the dowel pins you are looking at on McMaster?
 
.010 dowel clearance will allow you .010 runout if both holes are exactly the same distance apart. The thing about runout is that it doubles the position offset. What is the size of the dowel holes in the gear reduction? You can be reasonably sure that OxBox is holding the dowel holes to the input bore very close. I would think that they would be done in the same machining operation. According to the Machinery's Handbook you don't want more than .0016 interference with a cast iron OD. What is the PN of the dowel pins you are looking at on McMaster?

Don,

(Double Checks notes), misread McMaster, they are 0.6251 to 0.6253, which should be a reasonable press on 0.625 holes. Here is one example.

McMaster-Carr

The Allstar Hollow dowels should be here tomorrow and is the route I am likely to go. Putting a true press on them means I really don't want to take them out. I agree with your comment about the bolt clamping loads should be what keeps the box from rotating vs. the engine. Knocking them out after the box is installed is becoming more appealing.

The dowels are primarily there for alignment because they make the holes in the bell housing / gear reduction loose to make them assemble easily. There should be enough clamp force in the bolted joint that the dowels are not really doing anything after assembly. This is probably why you had your rogue dowel catastrophe. Your dowels were too much undersize.
 
Don,

(Double Checks notes), misread McMaster, they are 0.6251 to 0.6253, which should be a reasonable press on 0.625 holes. Here is one example.

McMaster-Carr

The Allstar Hollow dowels should be here tomorrow and is the route I am likely to go. Putting a true press on them means I really don't want to take them out. I agree with your comment about the bolt clamping loads should be what keeps the box from rotating vs. the engine. Knocking them out after the box is installed is becoming more appealing.
Gator, I think you got it handled.

Don
 
Gator, I think you got it handled.

Don
Thanks Don, I really appreciate the input and the thought that goes into it. So... come up with a reason to leave the dowels in once we are throwing prop??? :unsure:

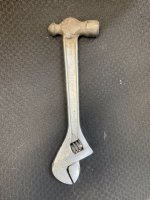
Allstar dowels measure 0.6215 and tap into the iron block easy with my smallest hammer wrench. Here is where I stand, 5/16 bolt head is smaller than dowel. It is inspectable. We will test knocking them out after loading the prop.

Hammer Wrench.jpeg

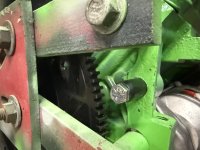
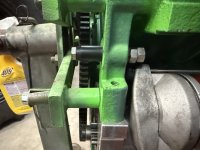
Gear Box Dowel #1.jpeg

Gear Box Dowel #2.jpeg

Gear Box Dowel #3.jpeg
 
Wouldn't a set screw in the block to lock it in place be a better answer?
Gary,

I did read your original message with the set screw suggestion, thanks for the input. I did/do agree that a set screw would resolve the stated problem.

To be clear, I do have a personal bias against set screws, primarily derived from trying to remove more than one from some rusted piece of crap. In particular the all-too-common situation of getting 3 out of 4 out after an hour, only to have to order another anyway.

In this case I would be drilling 2 blocks, 4 holes, all with a hand drill, likely after a drink or so. Now if I ever take them apart I gotta keep track of what dowel goes in what hole and then tap it in with perfect rotation to match up with the tapped hole.

The hollow dowel solution requires no modifications, is cheap, reproducible, interchangeable and reversable.

At this point I am mostly interested in the reversable aspect.
 
Maybe I'm lost but author customized an and ox and still accepted bad machine shop work after the fact and there is a go fund me page of what? More fails of stupid shit long past resolve decades ago?
That car motor guy needs to swap to ac or better yet gpu of ancient fixes?
Screw them dowl pins on motors and hold my beer?
I'd love a go fund me page for really good black rum but simpleton airboat shit is just that of live and learn, don't fuck up twice!
 
quite the thread! lol It never ceases to amaze me how much knowledge and experience there is on SouthernAirboat.com

and... it's been that way for years.

once i get my partybarge/duckblind completed here shortly, i will get back to getting the old gpu boat running the swamp again. haven't run it much since '23. I do enjoy reading about the big boy problems like dowel pins and gearbox woes. i'm gonna just get a hammer and knock the surface rust off my cage, put on some better blades, and drive it like it owes me money!!!!!!
 
Back
Top